Choosing the 2026 best plastic fabrication companies requires more than comparing polished websites. Global buyers need evidence of repeatable quality, transparent communication, and dependable delivery. A supplier may advertise advanced equipment, yet still struggle with tight tolerances or inconsistent material batches. The practical difference appears in production details.
This guide examines manufacturers that support injection molding, CNC machining, thermoforming, extrusion, and related services. It considers engineering capability, material knowledge, quality systems, tooling support, and international fulfillment. Readers should look for documented inspection procedures, clear sampling methods, and realistic production timelines. ISO certifications can add confidence, but they do not replace factory audits or verified customer references. Ask for dimensional reports. Review sample parts under normal lighting. Check how a supplier handles design changes, rejected components, and delayed shipments.
No ranking can fit every project. A medical enclosure, automotive trim panel, and retail display need different expertise. Cost alone can hide expensive rework, unclear tooling ownership, or weak after-sales support. Strong plastic fabrication partners explain those risks before accepting an order. That is a useful sign.
Some information may change during 2026. Capacity, certifications, pricing, and regional logistics are not permanent. We therefore treat this selection as a practical starting point, not a final verdict. Buyers should confirm current capabilities directly and request written quotations. Small mistakes happen. The important question is whether the supplier identifies them quickly, documents the cause, and improves the process. Reliable partnerships are built through that kind of honest evidence.
What Defines a Leading Plastic Fabrication Company in 2026
A leading plastic fabrication company delivers more than accurate parts. It demonstrates repeatable process control, documented material traceability, and practical engineering judgment. Buyers should expect dimensional inspection records, batch identification, and clear tolerance communication. These details matter when a molded housing must fit a metal insert without visible stress marks.
Digital capability is becoming measurable. The International Federation of Robotics reported that global factory robot installations reached 541,302 units in 2023. Plastic fabricators using automated inspection, machine monitoring, and predictive maintenance can reduce variation across large production runs. However, automation alone proves little. A poorly designed mold still creates expensive defects, only faster.
Environmental performance now requires evidence, not slogans. The OECD’s Global Plastics Outlook projects plastic waste could nearly triple by 2060 without stronger intervention. Leading suppliers therefore track recycled content, production scrap, energy use, and end-of-life options. Life-cycle data should identify assumptions clearly. Some recycled materials vary more than expected. That limitation deserves honest discussion.
According to Grand View Research, the global injection molding market is forecast to expand through 2030, increasing pressure on capacity and delivery reliability. Strong suppliers respond with validated tooling plans, backup processes, and realistic lead times. They also challenge drawings when a thinner wall, sharper corner, or unsuitable resin creates avoidable risk. That conversation may feel inconvenient. It often prevents failure later.
Plastic fabrication begins with matching geometry, volume, tolerance, and service conditions. CNC machining removes solid stock for precise prototypes and low-volume parts. Thermoforming heats sheet material over a mold. Injection molding suits repeat production with stable dimensions. Compression molding handles certain reinforced or heat-resistant components. Each process leaves different marks. In production reviews, I check draft angles, wall thickness, and cooling paths before tooling approval. A polished drawing cannot rescue poor material selection.
Material capability strongly affects performance. ABS offers practical impact resistance and easy finishing. Polycarbonate supports demanding impact applications. POM suits low-friction moving parts, while nylon handles strength and wear. Polypropylene resists many chemicals and repeated flexing. PVDF can serve harsh chemical environments. Glass fibers increase stiffness but may cause warpage or abrasive tool wear. UV stabilizers help outdoor parts, although testing remains necessary. Recycled content can reduce consistency between production lots.
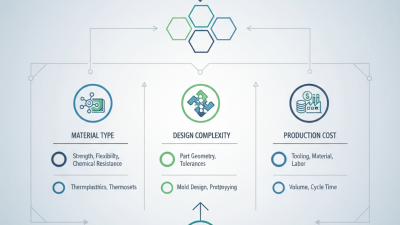
Global buyers should compare more than unit price. Ask for mold-flow analysis, first-article samples, and documented process windows. Sheet fabrication may combine sawing, bending, routing, and mechanical joining. Welded assemblies need careful joint design and leak testing. I once treated minor warpage as harmless. It became serious after assembly. That mistake changed my review checklist. Still, no checklist catches everything. Clear drawings and realistic tolerances matter. Supplier records should include material certificates, lot traceability, and dimensional inspection results.
Key plastic fabrication processes and commonly supported material families
Injection molding and extrusion support the broadest range of common thermoplastics. Blow molding is primarily used for hollow products, while rotational molding is frequently selected for large, durable polyethylene parts. Counts show the number of commonly used material families listed for each process and are not company rankings.
Evaluating a plastic fabricator requires more than comparing unit prices. Ask for material certificates, process capability records, and recent inspection reports. A reliable supplier should explain resin selection, mold design, tolerances, and expected shrinkage clearly. Request a sample made with the proposed production process. A polished prototype can hide weak mass-production controls. Measure wall thickness, hole positions, surface finish, and fit against your drawing.
Study the factory’s actual workflow. Review incoming-material checks, drying records, machine maintenance, and final inspection points. Ask how operators control moisture-sensitive plastics during humid weather. Small details matter. A missing drying log may predict bubbles, warping, or brittle parts. Verify that inspection tools are calibrated and nonconforming parts are quarantined. Photos help, but a live video audit or qualified local inspection provides stronger evidence. It is not perfect, yet it exposes gaps that brochures often hide.
Global sourcing also depends on communication and delivery discipline. Confirm drawing revision control, packaging tests, labeling, and export documents before placing a large order. Ask for a realistic lead-time range, not a hopeful date. Review how the fabricator handles tooling changes, recycled-content requests, and urgent quality claims. Test communication with a small pilot order. Fast replies do not always indicate strong engineering support. One supplier may respond quickly, then miss a critical tolerance question. Keep approvals, inspection photos, and corrective actions in one shared record.
Global buyers need more than a low unit price when selecting plastic fabrication companies in 2026. Regional capability often determines delivery stability, communication quality, and after-sales support. North American suppliers may offer strong engineering collaboration, rapid prototyping, and dependable domestic logistics. European manufacturers often emphasize material traceability, precise tolerances, and documented production controls. Asian production regions can provide broad molding capacity, competitive tooling, and scalable output. Each strength matters differently.
International coverage should be measured in practical terms. Can the supplier support technical calls across time zones? Does it provide drawings, inspection reports, and samples before mass production? A capable partner should explain resin grades, shrinkage risks, surface finishes, and acceptable tolerance ranges without hiding limitations. Local warehouses or regional service teams can reduce customs delays and simplify replacement shipments. Clear packaging standards also matter when parts travel thousands of kilometers.
Details reveal experience. Ask for a process flow, recent inspection records, and evidence of similar part geometries. Check how the company handles warped panels, short shots, color variation, or late tooling changes. These problems are ordinary in real production. A perfect supplier is unlikely. Some regional comparisons also become misleading because labor, freight, energy, and compliance costs vary widely. Buyers should compare total landed cost, not only the quoted factory price. Written communication can still fail across languages and cultures. Confirm every critical dimension twice.
2026 Best Plastic Fabrication Companies for Global Buyers
Quality begins with process control, not polished sales language. Experienced buyers should review material certificates, tolerance data, inspection records, and sample parts. Ask how operators manage warping, flash, surface defects, and dimensional drift during long production runs. A useful factory visit includes real work orders, calibrated measuring tools, and evidence of corrective actions. Details matter. No supplier is perfect.
Compliance requires more than sending a certificate by email. Confirm whether materials, labeling, documentation, and testing match the destination market and product application. Independent audits can verify quality systems, worker safety practices, and traceability. Keep approved drawings and revision records under controlled access. This reduces costly misunderstandings across time zones. Claims still need verification.
Sustainability should be measured through material yield, energy use, scrap recovery, packaging, and transport distance. Recycled content may reduce impact, but it can also affect strength, color, or consistency. Request lifecycle data and clear evidence instead of broad environmental promises. Cost analysis should include tooling, inspection, freight, duties, rework, and warranty exposure. The lowest quotation often hides risk. A better decision compares landed cost, production stability, and documented performance over time. Even careful forecasts can fail when resin prices or shipping schedules change. That uncertainty deserves a contingency plan.
| Evaluation Area | Buyer KPI or Dimension | Practical 2026 Reference Point | Evidence to Request | Cost and Risk Consideration |
|---|---|---|---|---|
| Quality Management | Quality management system | A current ISO 9001-certified quality management system is a widely recognized baseline for controlling documented processes, corrective action, supplier control, and internal audits. | Valid certificate, certification scope, issuing certification body, latest surveillance-audit status, and corrective-action records. | Reduces process variability and qualification risk, but certification alone does not guarantee product conformity. |
| Process Capability | Critical-characteristic capability | Cpk ≥ 1.33 is commonly used as a buyer requirement for stable critical characteristics; higher values may be specified for safety-critical or highly regulated applications. | Recent capability studies, control charts, measurement-system analysis, and the definition of critical dimensions. | Higher capability may require tighter process controls, additional inspection, better tooling, and higher unit cost. |
| Dimensional Control | Tolerance by fabrication process | Indicative values only: CNC plastic machining may commonly target approximately ±0.05 mm; injection-molded features often require design-specific tolerances around ±0.10–0.30 mm; thermoformed parts generally require wider tolerances because of material shrinkage and wall-thickness variation. | Part drawings with GD&T, process capability data, first-article inspection reports, and calibrated inspection-equipment records. | Very tight tolerances can increase tooling, machining, inspection, scrap, and rework costs. |
| Material Control | Resin and additive traceability | Each production lot should be traceable to the resin grade, colorant, additive package, supplier lot, processing date, and applicable certificate of analysis. | Material certificates, lot-control procedure, retained samples, formulation-change notification procedure, and chain-of-custody records. | Traceability supports recalls and compliance investigations; specialty resins and certified recycled content may increase material cost. |
| Regulatory Compliance | RoHS substance restrictions | For products within scope, the maximum concentration by weight in homogeneous materials is generally 0.1% for lead, mercury, hexavalent chromium, PBB, PBDE, DEHP, BBP, DBP, and DIBP, and 0.01% for cadmium, subject to applicable exemptions. | Supplier declarations, homogeneous-material assessments, test reports where appropriate, and exemption references when used. | Non-compliance can cause customs delays, product withdrawal, redesign, and liability exposure. |
| Chemical Compliance | REACH obligations | For products supplied into the European Economic Area, suppliers should assess substances of very high concern, communication duties, restricted substances, and applicable registration responsibilities. | Current REACH declaration, substance-disclosure statement, candidate-list review date, and safety information for relevant materials. | Formulation changes or substitute materials may affect color, strength, fire performance, tooling parameters, and price. |
| Product Safety | Application-specific testing | Testing should match the end use, such as flammability, chemical resistance, UV/weathering, biocompatibility, electrical safety, pressure performance, or food-contact requirements. | Test method, laboratory accreditation, sample conditioning, acceptance criteria, and complete test reports rather than summary claims. | Testing and certification should be budgeted during design; late failures can create major tooling and launch delays. |
| Environmental Management | Environmental management system | ISO 14001 certification provides a structured framework for environmental aspects, legal obligations, objectives, operational controls, and continual improvement. | Certificate, environmental policy, significant-aspect register, objectives, audit findings, and evidence of legal-compliance review. | Good environmental controls can reduce waste and disposal costs, although implementation may require investment in monitoring and infrastructure. |
| Carbon Transparency | Product carbon footprint | A credible product carbon footprint should define system boundaries, functional unit, data sources, allocation rules, electricity factors, transport, and end-of-life assumptions in line with ISO 14067 principles. | Product carbon-footprint study, calculation method, primary energy and material data, allocation policy, and independent verification where available. | Comparable carbon data improves sourcing decisions; recycled or low-carbon materials may have different performance and availability constraints. |
| Circularity | Recycled-content and recyclability claims | Recycled-content claims should distinguish pre-consumer from post-consumer material and identify the calculation method. Recyclability depends on polymer type, additives, contamination, local collection, and sorting infrastructure. | Mass-balance records, supplier certificates, material identification, design-for-recycling assessment, and substantiation for environmental claims. | Recycled content can reduce virgin-resin use but may affect color consistency, mechanical properties, odor, and process stability. |
| Waste Management | Scrap and regrind control | There is no universal acceptable scrap rate; buyers should require a documented 12-month trend by product and process, with clear rules for regrind use and disposal. | Scrap-rate records, nonconformance Pareto charts, regrind percentage, disposal manifests, and corrective-action reports. | Lower scrap improves yield and price stability; uncontrolled regrind can change strength, appearance, viscosity, and dimensional performance. |
| Supply Continuity | Capacity and lead-time reliability | Capacity should be demonstrated using available machine hours, tooling capacity, labor coverage, maintenance plans, and historical on-time-delivery performance rather than stated maximum output alone. | Capacity model, production schedule, on-time-delivery history, backup-equipment plan, business-continuity plan, and escalation contacts. | Lower quoted prices may be offset by missed launch dates, premium freight, expediting, or emergency tooling changes. |
| Tooling Economics | Tool ownership and lifecycle cost | The quotation should separate mold or fixture cost, engineering changes, maintenance, expected tool life, spare components, storage, and end-of-life responsibilities. | Detailed tooling quotation, tool drawings, maintenance schedule, cavity or station count, trial plan, and ownership terms. | Low initial tooling cost may result in higher maintenance, shorter life, more downtime, or greater piece-part cost. |
| Total Cost of Ownership | Landed cost rather than unit price | Compare piece price together with tooling amortization, packaging, inspection, freight, duties, currency exposure, payment terms, scrap, warranty risk, and expected service life. | Incoterms, price-validity period, material-price adjustment formula, packaging specification, freight assumptions, and warranty terms. | A transparent landed-cost model provides a more reliable comparison between geographically different supply options. |
| Documentation | First-article and change control | Production should not begin without an approved drawing revision, bill of materials, inspection plan, sample approval, and documented process-change notification requirements. | First-article inspection report, approved samples, revision-controlled documents, engineering-change procedure, and deviation-approval records. | Strong change control prevents unauthorized substitutions and reduces the risk of receiving parts that no longer meet the validated design. |
Note: The numerical values are industry reference points or regulatory thresholds, not universal guarantees. Final acceptance criteria should be defined in the drawing, purchase agreement, technical specification, and destination-market regulations.